APPLICATION · LABELS AND ADHESIVE TAPE
MULTI-CUT REFERENCE
IN LABEL AND TAPE SLITTING
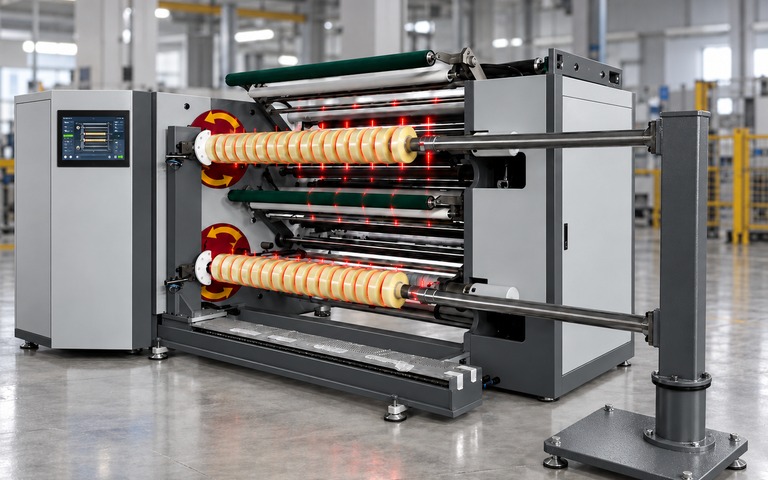
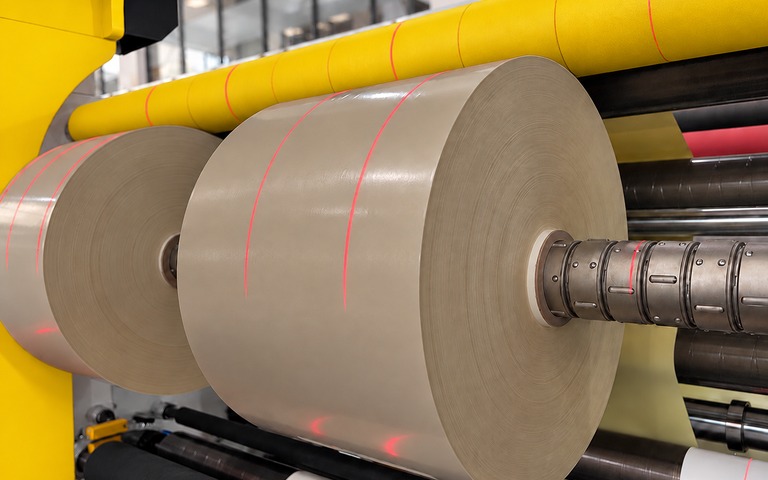
In narrow-web slitting, a single recipe means dozens of projected cutting references. Measuring and adjusting each one individually turns into the longest stop on the line. ServoMotion uses the shuttle architecture to set every blade position in sequence, and once setup is complete, all lines remain visible at the same time.
FROM THE FIELD
Application Images
ON THE LINE
DO THESE
SOUND FAMILIAR?
Measuring twenty blade positions one by one stretches the changeover well beyond the shift plan.
A millimetre of deviation on each slit adds up and becomes visible on the outermost cut.
As slit width falls, the same absolute error accounts for proportionally more scrap.
Position errors only come to light on the first product, when the cost has already been incurred.
WHAT WE MEASURE ON SITE
PARAMETERS THAT
DEFINE THE SYSTEM
The parameters below drive the design decisions in this segment. We measure these values on your line and base the quotation on that data.
| Number of simultaneous reference lines | The blade count in your densest recipe determines the number of carriages. |
|---|---|
| Slit width range | The narrowest slit determines line thickness and positioning tolerance. |
| Total working width | The widest recipe on the line determines travel range and rail length. |
| Changeover frequency | The number of changeovers per day forms the basis of the payback calculation. |
| Rail and traverse structure | The rail plane translates directly into positional accuracy. |
| Automation interface | Whether recipe data can be read from the line controller defines the integration scope. |
SYSTEM SELECTION
WHICH ARCHITECTURE
FOR THIS SEGMENT?
MOST APPLICATIONS
SHUTTLE PRECISOR
Slitting lines need dozens of reference lines visible at once. A single servo axis carries the laser carriages to their recipe positions in sequence; each carriage locks on the rail, and once setup is complete, all lines remain visible together.
Explore Shuttle Precisor →IF THE NUMBER OF PROJECTED LASER LINES IS LOW
CORE PRECISOR
If only a few reference lines need to be visible at the same time, an enclosed industrial profile may be sufficient at a lower investment. The decision is based on the densest recipe.
Explore Core Precisor →EXAMPLE INSTALLATION
SHUTTLE PRECISOR · 20 LASERS · 1,800 MM TRAVEL
One servo axis carries 20 carriages in sequence to the positions defined in the recipe. When the size changes, the operator simply selects the recipe. These figures come from one example installation; the dimensions for your line are determined during the site survey.
RELATED ARTICLES
WHAT WE HAVE
WRITTEN ON THIS
APPLICATION NOTE
REQUEST THE
APPLICATION NOTE
The application note is shared as a PDF on request.
LET'S ASSESS YOUR LINE TOGETHER
Share the number of simultaneous reference lines in your densest recipe and your working width, and we will define the carriage count and rail length together.